 Sankalp
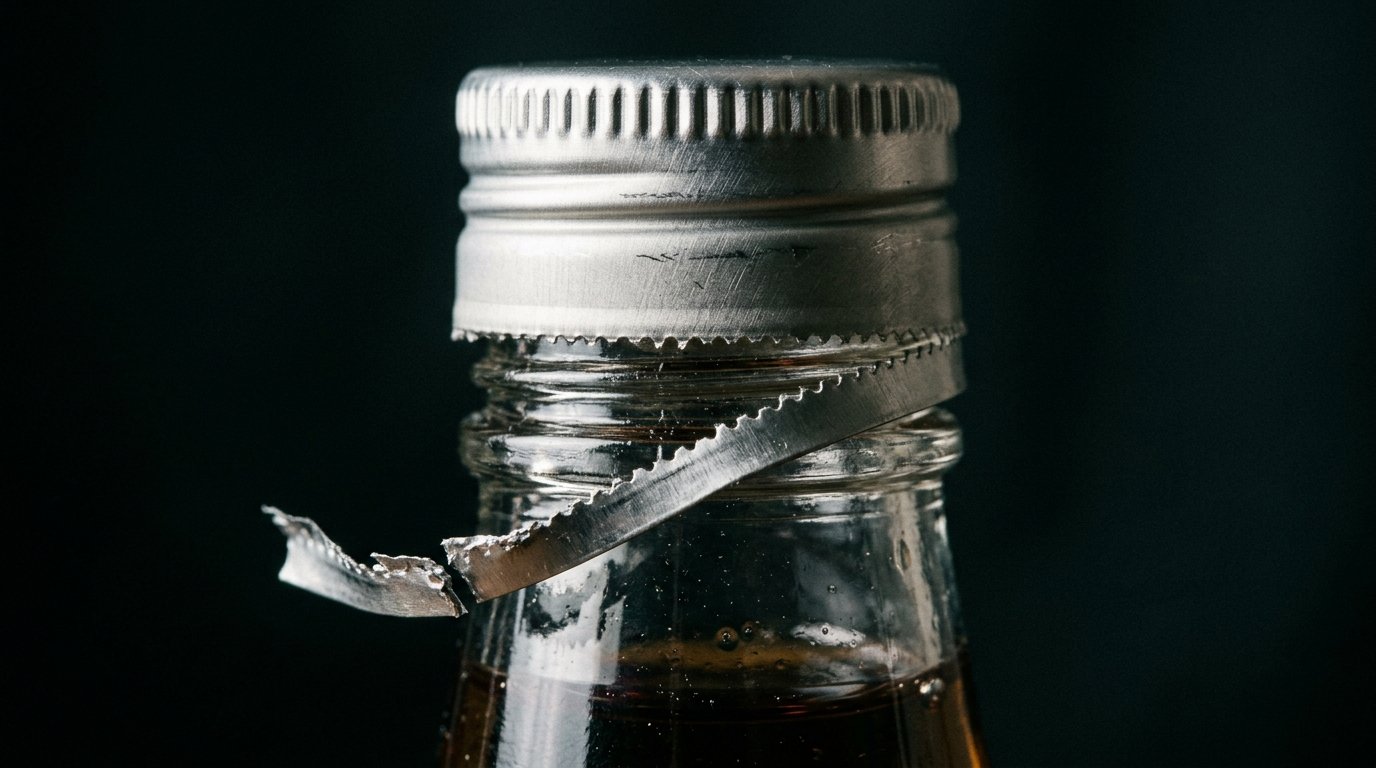
A tamper band fails in one of two directions, and they are opposites. It either breaks before the consumer opens the pack, which destroys the signal by making an untouched bottle look opened, or it does not break at all, which destroys the signal by making an opened bottle look untouched. Both trace to a narrow set of causes, and every one of them originates either in the cap as it was made or in the way the cap was applied. Splitting the investigation along that line is what makes it solvable.
The two failure modes are not equally serious
Premature failure is expensive. Failure to break is dangerous.
| Failure mode | What it looks like | Consequence |
|---|---|---|
| Premature break | Ring separated or bridges torn on packs that have never been opened, often visible in the case at the distributor | Stock rejected at trade level, consumer assumes tampering, brand carries the loss |
| Partial break | One or two bridges parted, the rest intact, ring hanging unevenly | Ambiguous signal that neither the trade nor the consumer can read |
| Failure to break | Cap turns off with the ring still attached and intact, ring rides up with the skirt | No tamper evidence at all, and the closure can be re-applied looking original |
The third row is the one that matters most. A band that never separates means the pack cannot report having been opened, which removes the entire function the closure was specified for. The distinction between what a tamper-evident closure actually promises and what buyers assume it promises is worth being clear about, and it is set out in tamper evident vs tamper proof.
Causes that originate in the cap
These are decided before the cap reaches your line, at design and at manufacture. They show up as a whole-lot pattern rather than as a head-by-head pattern.
| Cause | Mechanism | Sign in the pack |
|---|---|---|
| Slit and bridge geometry | Slits set where the ring parts; the uncut bridges between them carry the load. Number, length and placement decide how break force is distributed | Break behaviour uniformly too easy or too stiff across the whole lot, unrelated to which head applied it |
| Aluminium gauge | Thicker stock resists the forming rollers and needs more force to part; thinner stock parts readily but is exposed to handling damage | Whole-lot stiffness or fragility that does not respond to head adjustment |
| Scoring depth | The classic trade-off: too deep and bridges part in transit, too shallow and the ring survives the first opening | Deep scoring shows as separated rings in unopened cases; shallow scoring as caps removing with the ring attached |
| Ring variant choice | How the ring is configured against the skirt changes where and how it separates | A variant mismatched to the neck shows as a uniform, repeatable break problem |
| Lot-to-lot consistency | Gauge, temper and scoring have to hold across a production lot, not just within a sample | Break behaviour that shifts when a new carton of caps is opened |
Ring variant is a genuine design lever rather than a cosmetic option. R Vision’s Bev Cap is offered in Round Ring, Two Slit and Five Slit configurations. A continuous round ring and a ring divided by two or by five slits do not separate in the same way, because the slits determine where parting starts and how force is shared between the remaining bridge sections. If a line is fighting a break problem that follows the cap rather than the head, changing the variant is a legitimate step to try before changing the machine, and it belongs at the specification stage rather than after a lot has shipped.
R Vision’s water closure takes a different approach. Aqua Cap uses a three-part break-system ring, built so the break is unambiguous once it happens and cannot be reassembled. The mechanism is described in the three-part tamper break system.
Causes that originate in the application
These are decided on your line, in the seconds the capping head is working. They show up as a head-by-head or a lot-of-bottles pattern rather than as a whole-lot-of-caps pattern.
| Cause | Mechanism | Sign in the pack |
|---|---|---|
| Skirt roller pressure | Skirt rollers tuck the band under the neck bead. Too little and it never engages; too much and it is stressed or torn at the capper | Too little: cap removes with the ring riding up intact. Too much: rings already parted in the case |
| Roller profile and wear | A worn or wrongly profiled roller forms the band unevenly around the circumference | Uneven tuck, witness marks heavier on one side, breaks always starting at the same point |
| Capping head alignment | A cocked cap forms the band tight on one side and loose on the other | One or two bridges part on opening while the rest stay intact |
| Neck finish tolerance | The band locks under a bead on the bottle. An undersize or out-of-round bead gives it nothing to hold | Failures follow a bottle lot rather than a cap lot, across every head |
| Over-tightening | Excess top load and thread-roller pressure raise removal torque, so bridges see far more force than designed | High removal torque alongside rings that shatter rather than part cleanly |
| Handling after capping | Stacking load, vibration and rough case handling stress bridges already close to their limit | Rings intact at the line, parted on arrival |
The band is formed in the same stroke as the thread, by a separate set of rollers, which is why band problems and seal problems so often arrive together. The sequence is broken down in the ROPP capping process, and the neighbouring defects in common ROPP capping defects.
Telling the two apart in practice
One test separates cap causes from application causes, and it takes an hour.
- Pull twenty packs and record which head capped each one.
- Open them and record the outcome: clean break, partial break, no break.
- Failures clustered on one or two heads mean the cause is in the application. Look at roller pressure, roller wear and head alignment on those heads only.
- Failures spread evenly across every head mean the cause is in the cap or the bottle. Compare against a retained sample from a previous cap lot and a different bottle lot.
- Failures that follow a bottle lot across all heads and all cap lots point at the neck bead, not the closure.
Skipping step 3 is the common mistake. A cap lot gets rejected because the break rate looked high, when the whole of that rate sat on one worn roller.
What a band is supposed to do
The two failure modes above are only failures relative to a standard, so it is worth stating it. A tamper band has to survive filling, capping, casing, transport and shelf handling without parting, then part visibly and irreversibly on the first opening, in a way a consumer with no packaging knowledge can read at a glance. That is a narrow window, which is why band performance is a specification item rather than an assumption. The function is defined in what a tamper-evident cap is, and the resealing variant, where the ring stays with the bottle after the break so the cap screws back on, in resealable tamper-evident caps.
Frequently asked questions
Why do tamper bands break before the bottle is opened?
Because the bridges were weakened before they reached the consumer. The two common causes are scoring cut too deep at the cap manufacturer, which leaves bridges too fragile for transit, and skirt roller pressure set too high at the capper, which stresses or tears the band during application. Stacking load and rough case handling finish off bridges already close to their limit.
Why does a tamper band not break when the cap is removed?
Because it has nothing to lock against, or it was never tucked under the bead. Skirt roller pressure set too low leaves the band riding up with the skirt instead of locking under the neck bead, and a bottle finish with an undersize or out-of-round bead does the same even at correct settings. Scoring cut too shallow produces the same result across a whole cap lot.
Is the cap or the capping machine to blame?
Trace the failures back to the head that capped each pack. Failures clustered on one or two heads point to roller pressure, roller wear or head alignment. Failures spread evenly across every head point to the cap lot or the bottle lot instead. This one check resolves most disputes between a bottler and a closure supplier.
Does the number of slits in the ring matter?
Yes. The slits set where the ring starts to part and how break force is shared between the remaining bridge sections, so a continuous round ring and a ring divided by two or five slits behave differently on the same line. It is a design choice made at the specification stage, and worth revisiting if a break problem follows the cap rather than the head.
Can a broken tamper band be reattached?
A properly designed break cannot be hidden or reassembled, which is the point of the feature. Where a band appears to have resealed, it almost certainly never fully separated and the ring rode up with the skirt. That is a failure to break rather than a repaired break, it gives no tamper evidence at all, and it should be treated as a line fault.
To specify a ring variant against your neck finish and your capping head, or to trial Round Ring, Two Slit and Five Slit samples on your own line, contact R Vision.