 Sankalp
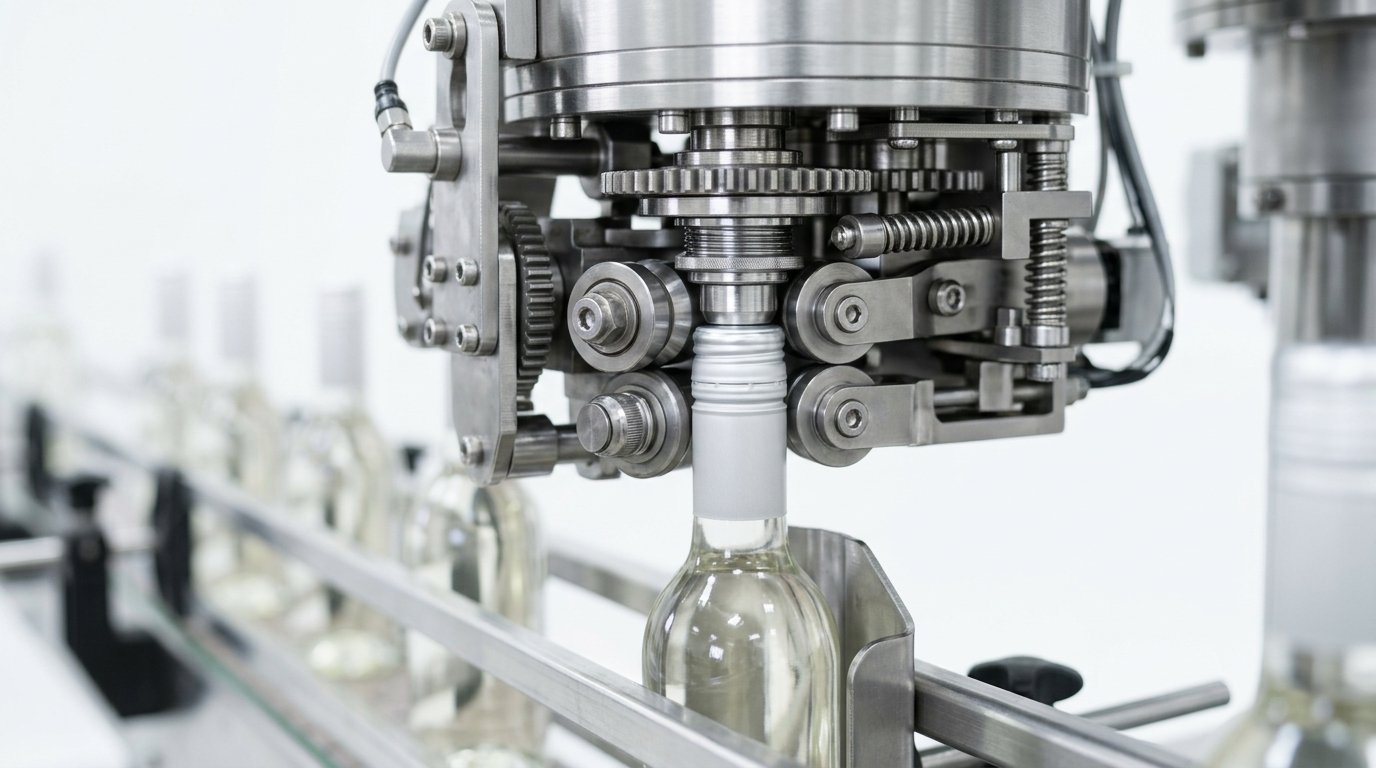
A ROPP capping machine takes a pre-formed aluminium shell, presses it onto a bottle finish, and uses rollers to form the thread and pilfer band directly against the glass or PET neck. The threads are created during capping, not moulded in advance. Three settings decide the result: the top load on the cap, the position and pressure of the thread rollers, and the position and pressure of the pilfer rollers.
What a ROPP capper actually does
An ordinary screw cap arrives with threads already moulded in. A ROPP shell arrives plain, a smooth aluminium cylinder with a liner inside. The machine does the forming work on the line. It seals the liner against the bottle mouth, then shapes the thread and the tamper band around the neck in one head cycle. Because the thread is formed to the exact profile of the bottle you are running, a correctly set ROPP head gives a tighter, more repeatable seal than a pre-threaded closure.
R Vision supplies the caps for this process, not the machine. Both R Vision products, the Aqua Cap for packaged drinking water and the Bev Cap for beverages, are 28/15 mm aluminium shells rated to 8 bar, so they suit standard 28 mm ROPP heads used across Indian bottling lines. To understand the closure side first, see what is a ROPP cap and parts of a ROPP cap.
The roll-on forming principle
Every ROPP head, from a hand tool to a high-speed rotary turret, works on the same two-part principle.
- A top-load pressure block (the thrust or knock-down block, sometimes called the chuck) pushes down on the flat top of the cap. This compresses the liner against the bottle finish and forms the seal. Seal quality is set here, by top-load pressure.
- Forming rollers then swing in against the spinning cap skirt. Thread rollers press the aluminium into the bottle’s thread profile. Skirt or pilfer rollers curl the lower edge under the locking ring to form the tamper band.
Get the balance between top-load and roller pressure right and you get a clean thread and a tight seal. Get it wrong and you get the defects covered in common ROPP capping defects. The step-by-step capping process breaks this sequence down further.
Machine types at a glance
| Machine type | Typical output | Best fit |
|---|---|---|
| Handheld / pneumatic hand tool | A few hundred caps per hour | Trials, lab batches, very small runs |
| Single-head semi-automatic | Roughly 600 to 2,000 bottles/hour | Small water and beverage brands starting out |
| Multi-head automatic (in-line) | Several thousand bottles/hour | Growing mid-volume lines |
| Rotary automatic turret | Tens of thousands per hour | High-speed established plants |
For a fuller breakdown of when to step up, read semi-automatic vs automatic cappers and the bottle capping machine buyer guide for India.
The settings that matter, and where each sits
A ROPP head has one axial setting and two sets of rollers, and each is set against the bottle’s neck finish rather than against the cap. The table below describes industry-typical practice. Numeric values are not given, because they depend on the finish drawing, the liner, the fill and the head make, and are established on the line during commissioning.
| Setting | What it does | Where it is set | Too low or too light | Too high or too heavy |
|---|---|---|---|---|
| Top load (chuck or head pressure) | Presses the cap down, compressing the liner onto the rim and shaping the top edge over the neck | An axial load on the pressure block, set by spring or pneumatic pressure on the head | Liner not compressed: leaks and lost carbonation | Crushed or buckled top, cocked cap, stress on the bottle neck |
| Thread roller position | Starts the thread at the right height | At the start of the bottle’s thread, following the thread down the neck | Misses the first turn of the thread: shallow or incomplete thread | Rolls into the top of the skirt: creasing and a distorted thread start |
| Thread roller pressure | Forms the aluminium into the thread profile | Radial pressure against the skirt | Shallow thread: cap loosens, spins or leaks under pressure | Aluminium over-worked: stripped or cracked thread, hard opening |
| Pilfer roller position | Tucks the band under the locking ring | Just below the locking ring on the neck | Band tucked too low or not under the ring: band slides off on opening | Rolls against the ring itself: band cut, bridges damaged |
| Pilfer roller pressure | Forms the band tightly under the ring | Radial pressure on the lower skirt | Band stands proud: cap opens without breaking the band | Bridges break at capping, so an unopened pack looks opened |
| Centring and neck grip | Keeps the head concentric with the neck and stops the bottle turning | Head-to-bottle alignment and the neck grip | Head off the neck axis or bottle slipping: tilted cap, uneven thread | Grip too tight: marked or distorted PET necks |
| Head speed and dwell | Gives the rollers time to complete their pass | Spindle speed and cycle time | Incomplete thread or band on some bottles | Scuffing of decorated skirts, extra wear |
Roller sequence matters as well. Published work on the roll-on process by Langley, Yoxall and Yates found that rolling the thread and the pilfer band at the same time can draw metal out of the first thread form, and that rolling the thread first removed the problem. In that study the capping head was calibrated to a load on the closure of 120 N, which is one calibrated line rather than a standard to copy. Why the opening force is measured as slip, bridge and over torque rather than as a single application torque is set out in cap torque specifications.
Where cap quality meets machine settings
A ROPP result depends on two things working together: the machine setup and the shell you feed it. Even a well-tuned rotary head cannot rescue an out-of-spec cap, and a good cap cannot fix a misaligned head.
- Machine responsibilities: top-load pressure, roller pressure, roller height, head-to-bottle centring, and spin speed.
- Cap responsibilities: consistent aluminium wall thickness, a true round shell, a correctly seated liner, and dimensional accuracy on the 28/15 mm finish.
R Vision’s Aqua Cap uses a three-part break-system tamper ring and a TPE liner suited to hot, cold, and carbonated fills. The Bev Cap uses a PVC-free TPE liner with a pilfer-proof ring that stays attached after opening. Consistency in these shells is what lets your line hold a single machine setting across a long run instead of re-adjusting every tray. See Aqua Cap vs ordinary ROPP caps for why shell consistency matters, and cap dimension tolerances and QC sampling for how to check a batch before it reaches the head.
Defects and their causes
Most ROPP faults have a machine cause, a cap cause and a bottle cause, and the fix depends on which one it is. The table below is industry-typical; a defect on nearly every bottle from the first of a run points to the caps or the bottles, while one that drifts in during a shift points to the machine.
| Defect | Machine cause | Cap cause | Bottle cause |
|---|---|---|---|
| Leak or lost carbonation | Top load too low | Liner missing, thin or off-centre | Chipped or uneven sealing rim |
| Cap spins, band does not break | Pilfer roller set too low or too light | Band bridges too strong for the ring | Locking ring shallow or out of tolerance |
| Band broken before opening | Pilfer roller too heavy, or riding on the ring | Bridges weak or damaged in transit | Locking ring oversize |
| Stripped or cracked thread | Thread roller pressure too high, or roller height wrong for the thread start | Gauge too thin for the finish | Thread profile sharp or damaged |
| Loose cap, shallow thread | Thread roller pressure too light | Gauge or temper inconsistent across the batch | Thread profile shallow or worn mould |
| Cocked or tilted cap | Head off-centre, worn pressure block | Out-of-round shell | Neck not square to the bottle |
| Crushed top or broken neck | Top load too high | Shell height wrong for the finish | Neck weak, or glass damaged |
| Creased skirt | Thread roller too high | Skirt too long for the finish | Finish shorter than drawn |
| Scuffed decoration | Dirty or worn rollers, excess speed | Print or coating under-cured | None |
The step-by-step fixes are in capping defects. Tamper band faults in particular, which run in both directions, are traced in why tamper bands fail, and leaks are read from the liner impression in why water bottle caps leak. Testing the capped pack for leak, torque and band break is covered in testing a ROPP closure.
Matching the machine to your closure
Before buying or renting a capper, confirm three things: the head is built for 28 mm ROPP (not crown or plastic screw), the top-load block suits your bottle finish, and the roller set matches your neck thread profile. Feeding a 28/15 mm aluminium shell like the Aqua Cap or Bev Cap through a head configured for a different closure is the most common source of early defects. If you are still choosing a closure, choosing caps for a water brand walks through the decision. Check the head against your bottle’s neck finish code too, because the roller set has to match the thread profile it is forming, and glass bottle neck finishes for ROPP caps lists the MCA finishes a 28 mm roll-on head works against, while neck finish standards on Indian glass bottles covers IS 7511 (Part 4), the Indian standard for roll-on pilferproof finishes. And if the closure supply itself is still open, how to choose a ROPP cap manufacturer in India sets out what to ask a maker before you order. The rest of the closure guides are indexed on the Learn hub.
What to specify when ordering caps for a given machine
Machine buyers are cap buyers, and a cap order that describes the machine saves a failed first run. Send the cap supplier these with the enquiry.
| Specify | Why it matters on the machine | Example |
|---|---|---|
| Cap diameter and height | Sets the pressure block and the roller heights | 28/15 mm |
| Neck finish and drawing reference | The rollers form against this profile | MCA 7.5 RF glass, or PET BPF |
| Skirt length against finish depth | A skirt too long creases, too short leaves the band short of the ring; see long skirt vs short skirt ROPP caps | Matched to the finish depth on the drawing |
| Head type and make | Confirms a roll-on head, not a crown or screw chuck | Single-head semi-automatic ROPP |
| Line speed | Affects dwell per cap and feed from the hopper | Bottles per hour |
| Fill and temperature | Hot, cold or carbonated fills load the liner differently | Carbonated, ambient |
| Liner | Must suit the fill and seal under the top load you run | TPE |
| Tamper band type | The pilfer roller is set to the band design | Three-part break system, or a ring that stays attached |
| Decoration on the skirt | Side print passes under the rollers and can scuff | Plain side, litho top |
| Sample quantity for a trial | Settings are established with the real cap on the real bottle | Enough caps for a commissioning run |
Frequently asked questions
Does R Vision sell ROPP capping machines?
No. R Vision manufactures the aluminium ROPP closures, the Aqua Cap and the Bev Cap, not the machinery. You source the capping machine separately from a machine builder and run R Vision caps on it.
What size ROPP head do R Vision caps need?
Both R Vision products are 28/15 mm aluminium shells, so they run on standard 28 mm ROPP heads used widely across Indian water and beverage lines. Confirm your head is set for ROPP rather than crown or plastic screw closures.
What forms the thread on a ROPP cap?
The thread rollers do. The cap arrives as a plain aluminium cylinder, and the machine’s thread rollers press that aluminium into the bottle’s thread profile during capping. The pilfer band is formed by separate skirt rollers in the same cycle.
Where should the pilfer roller be set on a ROPP head?
Just below the locking ring on the bottle neck, so it tucks the band under the ring. Set too low or too light, the band is not held and the cap can open without breaking it. Set too heavy, or riding on the ring itself, the bridges break during capping and an unopened bottle looks opened.
Can one machine run both Aqua Cap and Bev Cap?
Yes, as long as the head is set for 28 mm ROPP and centred to your bottle finish. Both products share the 28/15 mm format and the 8 bar rating, so the main change between them is the closure choice and the pilfer roller check for the ring design, not the machine type.
Why do I still get leaks with a good machine?
Leaks usually trace to top-load pressure or liner seating rather than the thread. An inconsistent shell or a poorly seated liner will leak even on a tuned head, which is why cap consistency and machine settings have to be right together.
Sources
- J. Langley, A. Yoxall and J. Yates, Understanding the roll-on-pilfer-proof process, 21st IAPRI Symposium, for head load, roller sequence and thread pull-out.
- CETIE, prevention of defects in aluminium screw caps, the bottling guide on identifying and correcting capping defects on roll-on closures.
Explore the caps that run on these machines: Aqua Cap and Bev Cap, or contact R Vision to discuss your line.