 Sankalp
A ROPP closure is qualified on filled, capped packs, not on loose caps. The core set is removal torque after a fixed dwell, a secure-seal test that pressurises the headspace, a leak test under vacuum or inverted storage, a drop test and a tamper band check, repeated after warm storage. Pull-up, the rotation check used on lug and plastic caps, has no equivalent on a roll-on cap because its thread is formed on the neck, so the formed thread and pilfer tuck-under are inspected instead. Acceptance is written against the closure’s rating and your own bottle, not copied from a universal table.
The tests at a glance
| Test | Equipment | What it measures | Acceptance is written as | A failure points to |
|---|---|---|---|---|
| Removal torque (slip and bridge) | Digital torque tester with a bottle clamp | How securely the cap was applied, and the effort to open it | A window set on your line at commissioning, read after a stated dwell | High: head load or roller pressure. Low: under-application, a lubricated finish, an uncompressed liner |
| Secure seal | Tester that pierces the closure through a sealed fitting and pressurises the headspace, pack under water | Pressure at which gas first escapes at the seal or thread | Holds an agreed pressure for an agreed time with no steady bubble stream | Bubbles at the rim: liner compression or rim damage. Cap lifting: thread form |
| Vacuum leak | Vacuum chamber, often with the pack submerged | Whether the seal holds when outside pressure drops | No liquid and no steady bubbles at the agreed vacuum and time | Liner seating, a chipped rim, a cocked cap |
| Inverted storage leak | Racks, absorbent paper, a warm room | Slow weeping a short test misses | No wet mark after the agreed period | Marginal compression, hot-fill vacuum on the seal |
| Drop | Drop rig or guided free fall onto a rigid surface | Whether an impact breaks the seal or moves the cap | No leak, cap not displaced, band intact | Skirt forming, pilfer tuck-under, shell gauge |
| Tamper band | Visual check, then bridge torque on opening | Band intact after capping and breaking on first opening | Every sampled band intact; every opened band broken | Pilfer roller setting, band geometry |
Removal torque, and what it is a measure of
Removal torque is the force needed to open a closed pack, and it is used as a check on application: whether the cap went on securely enough to seal and loosely enough to open. On a roll-on cap the first movement (slip torque) and the break of the pilfer bridges (bridge torque) are recorded separately.
Read after a stated dwell, because torque falls as the liner relaxes. Test hot-filled packs once cooled. Record head load and roller settings beside the readings, so drift traces to the machine rather than the cap. There is no universal torque table for ROPP; setting the window is covered in cap torque specifications, and CETIE publishes a removal torque test method for ROPP closures on glass as data sheet DT38.00.
A low reading on every head for one glass lot deserves a look at the bottle first, because lubricating coating on the finish lowers friction, as cold-end and hot-end treated glass explains.
Pull-up, and why a roll-on cap has none
On a lug cap or a pre-threaded plastic closure, pull-up is where the cap stopped turning, measured against a reference on the bottle finish such as the mould seam. It is a quick, non-destructive proxy for how far the cap was turned down.
A ROPP cap arrives with no thread. Rollers press the aluminium into the bottle’s own thread and tuck the band under the locking ring, so there is no thread position to read. The checks that take its place look at what was formed: an even, continuous impression ring in the liner, a clean thread on the skirt, the band tucked under the ring all round, and the cap at the right height. A cap sitting high or low usually means the skirt does not suit the finish depth, which long skirt vs short skirt ROPP caps explains.
Secure seal testing
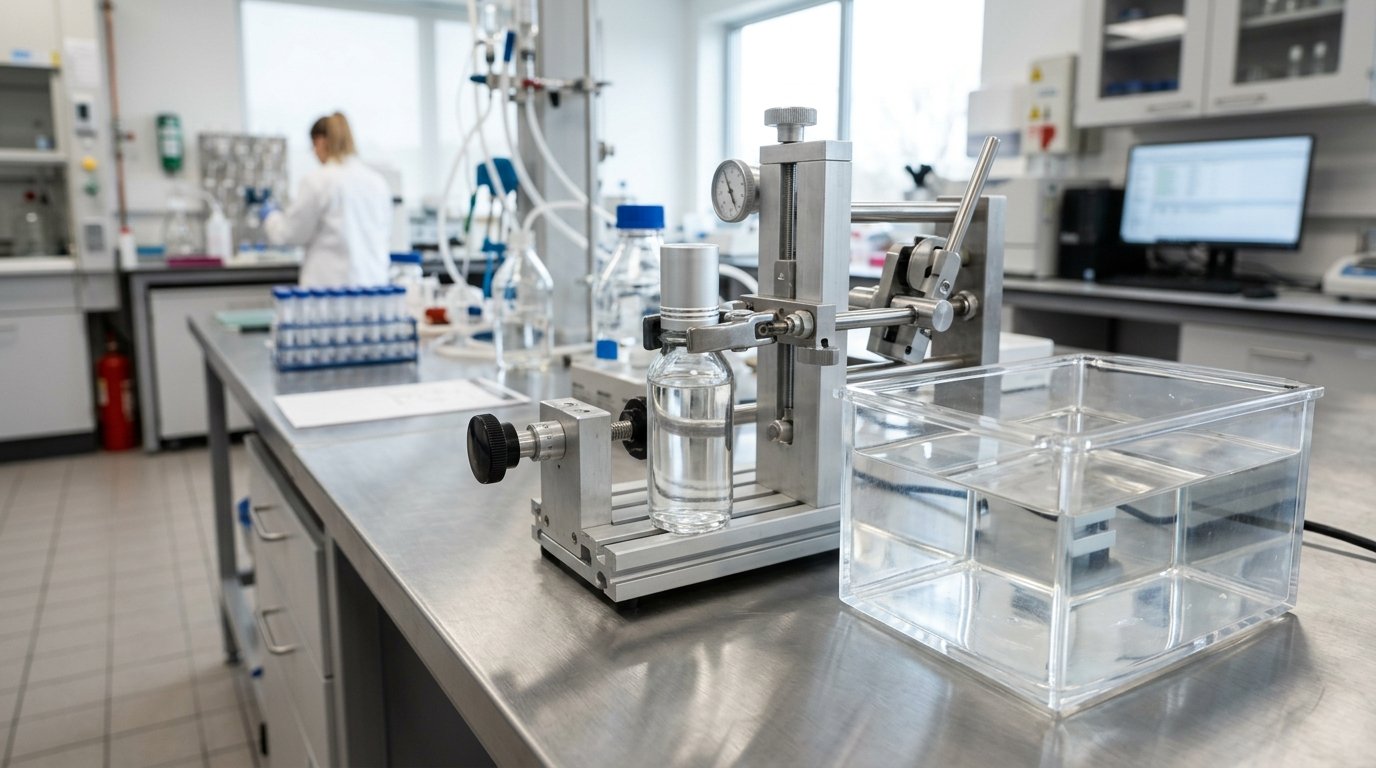
A secure-seal test checks the seal with gas rather than liquid, which makes it more sensitive than watching for drips. It is what most buyers mean by a ROPP closure tester.
Set the test pressure between two limits: above the pressure the filled pack reaches in warm storage, and no higher than the lower of the closure’s rating and the bottle’s. For a carbonated line on a closure rated to 8 bar, work out your drink’s storage pressure at warehouse temperature first. Record the pressure at which the seal first vents as well as the result, because a falling venting pressure across lots is an early warning.
Leak and drop testing
A vacuum test finds a weak seal in minutes; an inverted storage test in a warm room finds the slow weeper that passes every quick test. Plastic water containers already carry both a leakage and a drop test in their own standard: IS 15410 calls up the methods in IS 2798, holds containers upside down for the leakage test, and sets 0.5 m as the drop height for a 20 litre container. A closure test on your line adds the cap and the capping head to that.
For the drop, use set orientations, usually base, side and cap-down, from a height matched to the worst fall between filler and shelf, and keep it fixed so lots compare. ASTM D5276 describes drop testing of loaded containers by free fall. When packs leak, why water bottle caps leak traces the cause from the impression ring, and why tamper bands fail covers a band that splits.
The incoming test sequence
Run non-destructive checks first and destructive tests last, so each sampled pack gives the most information before it is used up.
| Step | What you do | Why here |
|---|---|---|
| 1 | Check lot paperwork against the order | A wrong lot fails every later test |
| 2 | Draw the sample to your sampling plan | The plan decides how many caps count as evidence |
| 3 | Measure and inspect empty caps | Separates dimensional faults from capping faults |
| 4 | Cap your own bottles on your own line | A roll-on cap is only finished once applied |
| 5 | Inspect thread form, tuck-under and impression ring | Non-destructive, and explains later results |
| 6 | Removal torque after the stated dwell | Opens the pack |
| 7 | Secure seal on a separate set | Destroys the closure |
| 8 | Vacuum or inverted leak | Needs unopened packs |
| 9 | Drop, then leak-check the dropped packs | Impact first, then its effect |
| 10 | Warm storage, then repeat steps 6 to 8 | Carbonated and hot-filled packs are weakest after storage |
Sample sizes and accept or reject numbers come from the plan; cap dimension tolerances and QC sampling covers the measurement list and AQL sampling, and quality certificates to ask your cap supplier for the paperwork for step 1. Failures that cluster on particular capping heads are the machine, which common ROPP capping defects maps; failures spread across all heads from the first pack of a lot point to the cap or the bottle.
R Vision’s Aqua Cap and Bev Cap are 28/15 mm aluminium ROPP closures with a TPE liner, rated to 8 bar, running on standard roll-on application machinery and adhering to USFDA and EU standards. To run samples through these tests on your line, contact R Vision.
Frequently asked questions
What is a ROPP closure tester?
It usually means a secure-seal tester: an instrument that pierces a capped closure through a sealed fitting, holds the pack under water and pressurises the headspace to find the pressure at which the seal or thread lets gas escape. A full bench adds a digital torque tester for slip and bridge torque, a vacuum leak chamber and a drop rig.
What does removal torque measure?
The rotational force needed to open a closed pack. It is used as a check on how the closure was applied: too high means over-application or a pack that is hard to open, too low means the cap may not have been compressed enough to seal. Read it after a stated dwell, because torque falls as the liner relaxes after capping.
Is pull-up measured on ROPP caps?
No. Pull-up measures where a pre-threaded lug or plastic cap stopped turning against a reference mark on the bottle finish. A ROPP cap has no thread until the capping head forms one on the neck, so there is no position to read. The formed thread, the band tuck-under and the liner impression ring are inspected instead.
How many caps should I test from an incoming lot?
The sampling plan decides it. In India, attribute sampling for lot-by-lot inspection follows IS 2500 (Part 1), identical with ISO 2859-1: the sample size comes from the lot size and the inspection level, with general inspection level II used unless the specification says otherwise. Agree the plan and the acceptance quality limit with the supplier in writing.
Sources
- CETIE general data sheets: DT38.00, roll-on pilferproof closure removal torque test method, and DT15.53, leakage test procedure.
- IS 15410: 2003, containers for packaging of natural mineral water and packaged drinking water, BIS, for the leakage and drop test clauses.
- ASTM International, D5276, drop test of loaded containers by free fall.
- IS 2500 (Part 1): 2000, attribute sampling plans indexed by AQL, BIS, and ISO 2859-1:1999.