 Sankalp
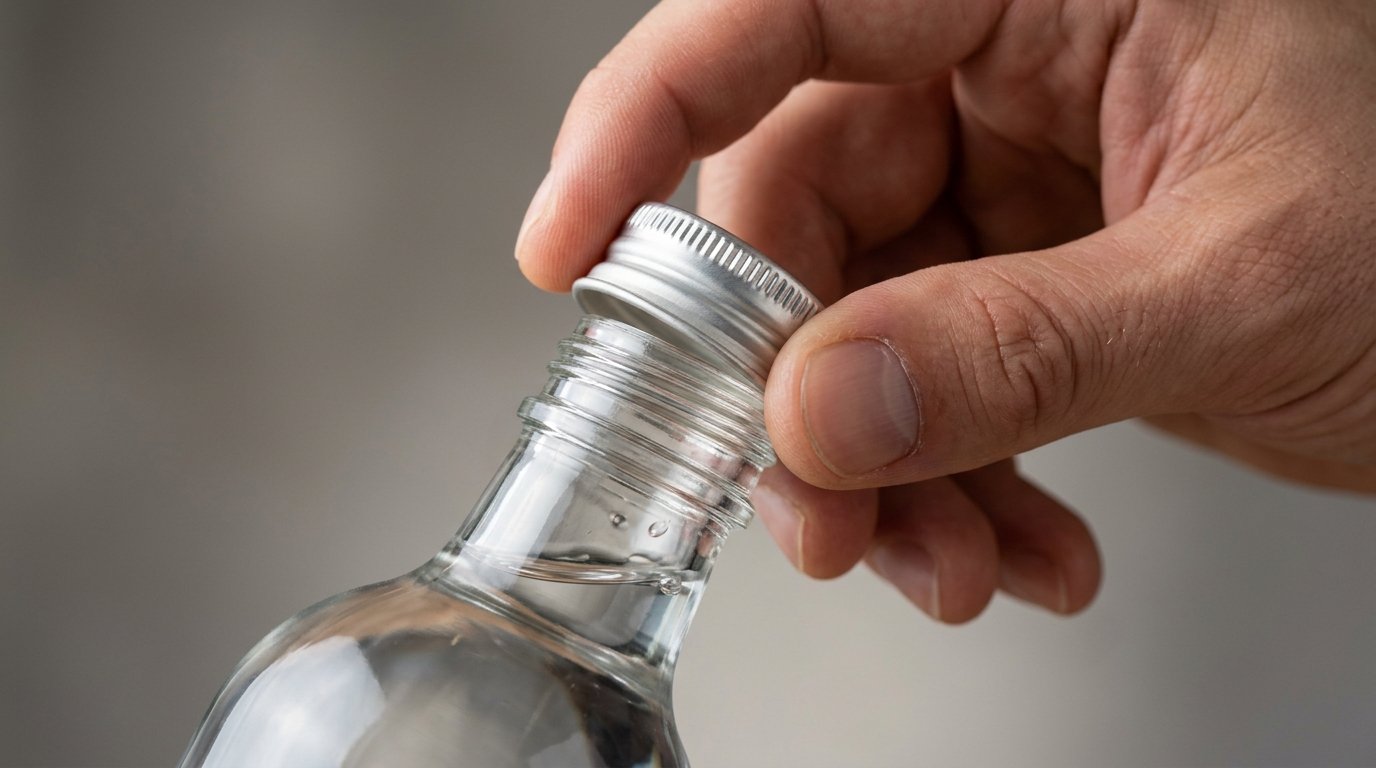
Application torque is the twisting force a capping machine puts into a closure. Removal torque is the force needed to open it later, and it is the lower of the two, because the liner relaxes after capping. That is the picture for a pre-threaded screw cap. A ROPP cap does not work that way: it arrives with no thread, and its thread is formed by rollers pressing aluminium into the bottle’s own profile. On a ROPP line you control capping head load and roller pressure, and you measure opening torque.
Key takeaways
- Removal torque is measured, not derived. Its relationship to application torque is not linear.
- Torque decays after capping as the liner conforms to the finish, so removal torque is measured after a defined dwell.
- A ROPP closure has no application torque in the screw cap sense. Roller pressure and head load are the equivalent controls.
- Torque values are specified per bottle, per liner and per line.
Application torque and removal torque on a threaded closure
Industrial Physics defines application torque as the torque delivered by the capping machine to fit the closure during filling and sealing, and removal torque as the rotational force required to unscrew and open it. They are not one measurement taken twice: application torque is a machine setting verified at the head, removal torque a package property verified on a filled pack. The method most cited is ASTM D3198, which ASTM withdrew in 2016.
Torque decay, and why the interval is part of the spec
After a closure is applied, the liner conforms to the container finish and internal stresses dissipate, so removal torque falls over the first hours. A reading at the head will not match one taken later, which makes “removal torque” meaningless without a stated interval. Industrial Physics recommends conditioning samples at ambient temperature for a defined dwell, typically a minimum of 30 minutes to several hours depending on the protocol. Bottle cap liner materials covers how compounds behave under load.
Why a ROPP cap is a different problem
A ROPP closure leaves the factory as a plain aluminium shell with no thread. During capping the head presses down and a spring pivot system moves rollers inward; two thread rollers form the thread profile using the glass finish as a mandrel, and two pilfer rollers tuck the band under the locking ring. The ROPP capping process sets out that sequence, and what a ROPP cap is covers the format. None of it is a twisting force applied to a finished thread, so there is no application torque to specify. Head load and roller pressure take its place, both commissioning settings rather than properties of the cap.
Work published at the 21st IAPRI Symposium by Langley, Yoxall and Yates puts numbers on it. Their capping head was calibrated to a load on the closure of 120 N, on lines that typically cap 300 to 400 bottles per minute, and halving that load to 60 N did not degrade sealing to the point of leakage. Higher roller pressure raised liner compression and gave a more defined thread form and pilfer tuck-under, yet opening torque showed no correlation with it. They also identified thread pull-out, where cap material is drawn out of the first thread form to make the second when thread and pilfer roll together, which rolling the thread first eliminated.
The torque vocabulary that applies to ROPP
Because the closure is formed in place and carries a tamper band, opening a ROPP cap is a sequence of events rather than one unscrewing.
| Term | What it measures |
|---|---|
| Slip torque | Torque required in opening to make the initial movement, the very first slip |
| Bridge torque | Torque required in opening to break the pilfer bridges between cap and band |
| Over torque | Torque required to turn the closure the wrong way and strip the thread |
| Removal torque | What the consumer experiences, dominated by whichever of slip or bridge torque is higher |
The design target is counterintuitive: over torque should be high, so a cap turned the wrong way resists rather than strips, while slip and bridge torque stay low enough for the pack to open comfortably. Bridge torque stayed the higher of the two in those tests, which makes pilfer band geometry the thing to attack when a pack opens too hard.
Under-torque and over-torque as line faults
| Fault | What you see on the pack | Where to look first |
|---|---|---|
| Under-torque | Leakage, lost carbonation, tamper feature not properly formed | Head load too low, worn liner seat, cap cocked at pick-up |
| Over-torque | Stripped thread, scored cap, pack the consumer cannot open | Roller pressure too high, roller position or height off |
| Spinner | Cap turns without breaking the pilfer band | Pilfer tuck-under incomplete, locking ring geometry |
None of these is diagnosed from a torque reading alone. The reading says the pack is out of window; the ROPP capping machine guide and capping defects say which setting moved.
What to specify, and what not to ask for
There is no universal torque table for ROPP, and a supplier who hands you one has guessed. The values depend on the neck finish, the liner, the fill, the head load and the roller set. Instead:
- Agree the protocol first: which torques, at what dwell, on how many packs per shift.
- Establish the window on your own line during commissioning, with the actual bottle, liner and fill.
- Re-establish it whenever the bottle changes, because a new finish drawing invalidates the old window.
- Record head load and roller settings alongside the readings, so drift traces to the machine rather than the cap.
R Vision’s Aqua Cap and Bev Cap are 28/15 mm aluminium closures with a TPE liner, rated to 8 bar, running on standard roll-on machinery and adhering to USFDA and EU standards.
Frequently asked questions
What is the difference between application torque and removal torque?
Application torque is the twisting force the capping machine puts into the closure during filling and sealing. Removal torque is the force needed to unscrew and open the pack afterwards, and it is lower, because the liner conforms to the finish and internal stresses dissipate. The relationship is not linear, so removal torque must be measured, not calculated.
Do ROPP caps have an application torque?
Not in the usual sense. A ROPP closure has no thread when it reaches the capper. The head presses down on the plain shell and rollers form the thread against the bottle’s own profile, so there is no pre-formed thread to twist onto a neck. The equivalent settings are head load and roller pressure.
How is a ROPP cap’s opening force measured?
By recording the opening events separately: slip torque, the force to make the very first movement, bridge torque, the force to break the pilfer bridges between cap and band, and over torque, the force to turn the cap the wrong way and strip the thread. Bridge torque is usually the higher figure.
What torque should I set on my capping line?
There is no single answer, and a supplier quoting one without seeing your bottle is guessing. The window depends on the neck finish, the liner, the product, the head load and the roller setup. Establish it during commissioning with the actual bottle and fill, and again whenever the bottle changes.
Sources
- Industrial Physics, Torque testing explained, for the definitions, relaxation and dwell conditioning.
- ASTM International, D3198, Application and Removal Torque of Threaded or Lug-Style Closures, withdrawn 2016.
- J. Langley, A. Yoxall and J. Yates, Understanding the roll-on-pilfer-proof process, 21st IAPRI Symposium, 2003, for head load, roller mechanics and torque definitions.
- CETIE, prevention of defects in aluminium screw caps.
R Vision Pvt. Ltd manufactures 28/15 mm aluminium ROPP closures from Sinnar, Nashik. To set a torque window on your line, use contact us.